Concrete Pump Parts Knowledge
Concrete Pump Hydraulic Oil Foaming: Aeration, Cavitation, and Fault Diagnosis
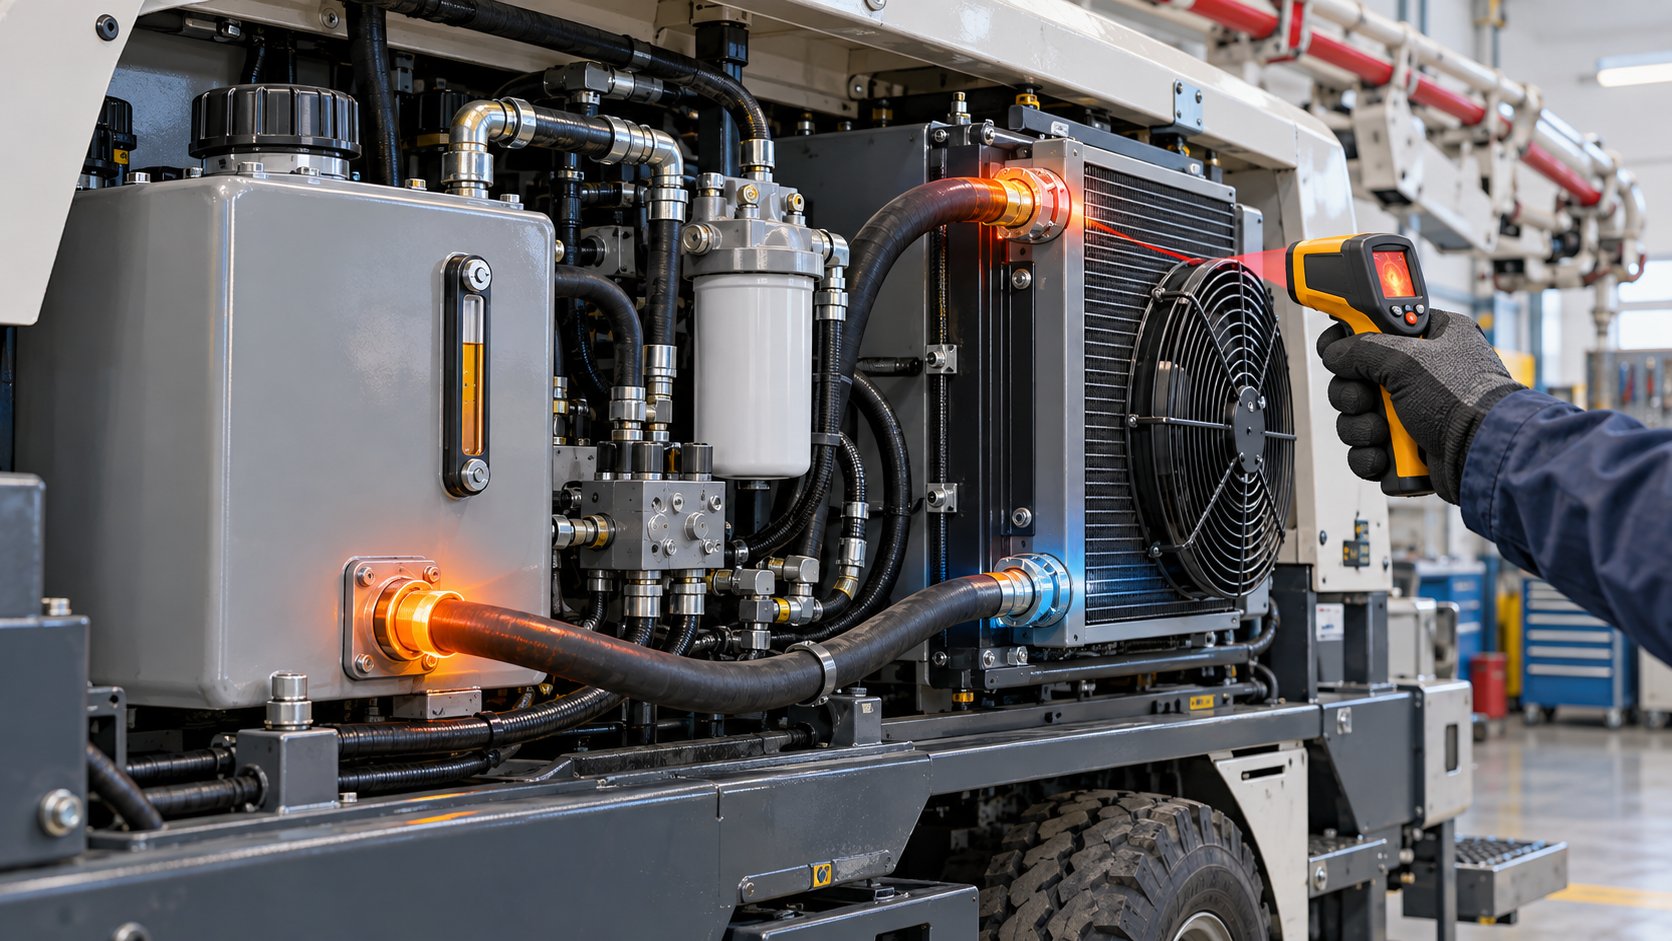
Foam in a concrete pump hydraulic reservoir is evidence that gas is being trapped in or released from the oil, but it does not identify the root cause by itself. The system may be drawing air through a suction-side leak, agitating return oil, operating with an incorrect level, struggling with an inlet restriction, or using fluid that cannot release air fast enough under the actual operating conditions.
The useful diagnostic question is not simply “Why is the oil foamy?” It is: Is the observation surface foam, entrained air, cavitation, or a water-contaminated emulsion—and where did that condition begin? The answer determines whether the next check belongs at the reservoir, pump inlet, return circuit, recent service work, or fluid sample.
Why does hydraulic oil foam in a concrete pump?
Hydraulic oil foams when bubbles reach the reservoir surface and remain there instead of collapsing promptly. Air can enter through an imperfect pump-inlet connection, be mixed into the fluid by a return line or low oil level, or remain suspended because the oil, contamination, temperature, and reservoir residence time do not allow it to separate quickly.
Concrete-pump OEM troubleshooting information treats air entry as a real hydraulic fault. The Multiquip Mayco LS300G operation manual lists air in the system, reservoir aeration, a vacuum leak in the suction line, insufficient oil, and a closed suction strainer among checks for a noisy main hydraulic pump. That sequence matters: noise and foam can share a cause, but neither proves that the hydraulic pump itself must be replaced.
Danfoss explains the underlying mechanism in its hydraulic-fluid technical information. Air increases fluid compressibility, which can make a system less responsive, noisier, hotter, and more difficult to control. The same document distinguishes air release—the time needed for bubbles within the fluid to reach the surface—from the fluid’s foaming behavior at the surface.
Foam, aeration, cavitation, and milky oil are not synonyms
These observations are often grouped together in a work order, yet they describe different conditions. A technician should record what is visible before draining the tank or replacing parts.
| Observation | What it means | First evidence to collect |
|---|---|---|
| Stable foam layer on the reservoir surface | Bubbles have reached the surface but are not collapsing quickly; air entry, turbulence, oil condition, or fluid chemistry may be involved | Oil level, return-flow disturbance, recent top-up or oil change, foam persistence after shutdown |
| Cloudy oil filled with fine moving bubbles | Air is entrained below the surface; it may be circulating back to the pump before it can separate | Suction connections, reservoir flow pattern, pump noise, cylinder response, changes with temperature |
| Sharp pump noise with restricted inlet conditions | Cavitation or inlet starvation may be occurring; dissolved gas or vapor can form cavities under low inlet pressure | Oil level, suction valve position, strainer condition, hose collapse, cold-oil behavior, OEM inlet-pressure checks |
| Opaque or creamy fluid that does not clear like fine bubbles | Water contamination or an emulsion is possible; appearance alone is not a laboratory diagnosis | Settling sample, laboratory test where approved, breather condition, wash-water entry, condensation history |
| Large bubbles immediately after hydraulic work | Air may be trapped in a line or component that was opened | Exact components disturbed, refill method, model-specific bleeding procedure, change in oil level as actuators cycle |
Do not diagnose water solely because oil looks pale. Fine entrained air can also make normally translucent oil appear cloudy. Conversely, a clear surface does not prove that the circulating fluid is free of small bubbles.
Where can air enter the hydraulic circuit?
1. Pump suction connections
A suction-side joint can admit air without producing the external oil leak that technicians expect from a pressure line. The pump inlet operates below reservoir pressure, so a damaged seal, loose clamp, cracked hose, porous hose wall, or disturbed fitting can draw air inward. Danfoss identifies insufficiently tight suction-line seals and fittings as a typical air-entry path.
Inspect the complete inlet route from reservoir to pump. Pay particular attention to work performed immediately before the symptom began. A hose replacement, strainer service, oil change, pump installation, or reservoir cleaning can introduce a new sealing, routing, or priming problem. Do not tighten fittings indiscriminately; verify the connection type and use the applicable installation procedure and torque.
2. Low oil level and reservoir vortexing
Oil level must be checked with the machine in the state specified by its manufacturer. Cylinder positions, accumulator condition, temperature, and deployed functions can change the reservoir level. A reading taken in the wrong configuration can lead to underfilling or overfilling.
If the suction region forms a vortex or intermittently draws surface air, topping up may remove the immediate symptom—but the cause of the low level still has to be found. External leakage, an incorrect service fill, trapped oil elsewhere in the circuit, or a misleading reading condition can all produce the same low-level observation.
3. Return oil entering above the fluid surface
High-velocity return oil can entrain air when it splashes into the reservoir or creates strong surface agitation. Reservoir baffles, diffusers, and separation between return and suction zones help provide time for bubbles to leave the oil before it is drawn into the pump again. Danfoss’s mobile-hydraulic design guidelines describe submerged return and inlet lines, separation between them, and reservoir residence time as controls for aeration.
A return-tube problem is not the only explanation for turbulence. An incorrect oil level, missing internal component, changed hose routing, excessive return flow, or component leakage can alter the reservoir flow pattern. Compare the current arrangement with the machine’s parts book and hydraulic schematic.
4. Inlet restriction and cold, viscous oil
A blocked or closed suction strainer, collapsed hose, partly closed valve, undersized replacement line, obstructed breather, or oil that is too viscous at startup can starve the pump inlet. The result may be abnormal noise and bubbles, but the correct response is not automatically to install a new pump.
Record whether the noise and cloudy appearance are strongest after a cold start and decrease as the oil warms. That pattern can support an inlet-restriction or viscosity hypothesis, but it does not prove one. Confirm the oil grade, ambient range, warm-up method, strainer arrangement, and inlet test procedure for the exact machine. Do not transplant a fluid specification or cold-start rule from another brand or model.
Why can the pump become noisy or the valve shift erratically?
Liquid transmits hydraulic power with relatively little compression. Entrained air changes that behavior. Instead of actuator motion following oil delivery cleanly, part of the input first compresses the gas. The operator may notice delayed response, irregular movement, a different sound, or an unstable pressure indication.
On a concrete pump, those symptoms can appear during drive-cylinder reversal, agitator operation, or distribution-valve movement. However, aerated oil is only one possible cause. A Concrete Pump Slewing Cylinder that shifts inconsistently should not be condemned from reservoir foam alone. The command signal, accumulator or supply circuit where fitted, directional valve, hose routing, linkage resistance, cylinder bypass, and S-valve or rock-valve mechanism still require model-specific checks.
The practical lesson is to connect sound, reservoir appearance, operating state, and inlet conditions before deciding which component has failed. Cloudy oil and abnormal noise are observations; neither identifies the failed part without suction, fluid, and circuit evidence.
Can adding antifoam solve the problem?
Do not add an aftermarket antifoam product unless the equipment and fluid suppliers have approved it in writing. A fluid formulation balances air release, foam control, filterability, water separation, seal compatibility, wear protection, and viscosity behavior. Altering one property in the reservoir can interfere with another.
Shell’s Tellus S4 VE technical page identifies air release and foam control as hydraulic-fluid performance considerations. Those are formulation properties, not a field invitation to dose the reservoir by guesswork.
If foaming follows an oil change or top-up, document every product name, viscosity grade, approval, batch if available, and quantity added. Mixing individually acceptable fluids can still produce uncertain compatibility or air-release behavior. Ask the pump manufacturer and lubricant supplier whether the mixture is approved and what sampling or change procedure they recommend.
A diagnostic workflow for foamy or aerated oil
- Define the observation. Photograph the sight glass or reservoir safely. Record whether bubbles are on the surface, dispersed through the oil, or accompanied by an opaque emulsion.
- Record the machine state. Note ambient and oil temperature, engine speed, pumping output, active function, cylinder positions, slope, and time from startup.
- Make the system safe. Stop the machine and control hydraulic, accumulator, concrete-line, and mechanical stored energy according to the OEM procedure. The ACPA maintenance-safety guide is a useful industry reference.
- Check oil level correctly. Use the specified machine position and temperature. Identify why the level is incorrect before treating a top-up as the complete repair.
- Inspect the suction route. Check disturbed joints, seals, clamps, hoses, valves, strainers, and breather condition. Look for hose softening or collapse as well as external leakage.
- Review recent work. Compare the installed filter, hose, seal, pump, and fluid with the service record and parts documentation.
- Observe how the condition changes after shutdown. Record how quickly visible bubbles clear. Do not use a generic clearing-time limit as a pass/fail rule; fluid, temperature, contamination, and reservoir geometry differ.
- Separate air from water and solids. Take a representative sample using the machine and laboratory procedure. A jar photograph alone cannot quantify water, particle count, viscosity, or additive condition.
- Test under a controlled, approved condition. After correcting an identified fault, repeat the same operating state and compare noise, response, temperature, and reservoir appearance.
Never open a pressurized hydraulic line to “bleed the air” unless the manufacturer’s procedure explicitly requires work at that point and provides the necessary safety controls. High-pressure oil injection injuries can appear minor at the skin while causing severe internal damage.
What should a fluid sample and service record include?
A useful sample record links laboratory data to the operating event. Record the oil manufacturer and product, viscosity grade, equipment hours on the oil, total reservoir capacity, top-up history, sampling point, oil temperature, machine state, and the symptom present at the time. Also record whether the sample was taken before or after the filter and whether the line was flushed before collection.
Depending on the problem and the laboratory program, relevant tests may include viscosity, water content, particle count, elemental analysis, oxidation indicators, and air-release or foaming evaluation. The equipment manufacturer and lubricant supplier should determine which tests and limits apply. There is no universal visual color, bubble count, or foam height that can replace the specified analysis.
What information is needed before ordering parts?
If the diagnosis identifies a hose, suction seal, strainer, breather, filter, reservoir component, pump, or actuator fault, send the supplier more than the machine brand. Provide:
- concrete-pump manufacturer, model, serial number, and year;
- complete installed part numbers and revision marks;
- hose length, internal diameter, pressure/vacuum suitability, end connections, and routing photographs;
- filter or strainer housing and element numbers;
- reservoir port, standpipe, diffuser, baffle, and breather details where relevant;
- hydraulic-pump identification plate and shaft/port configuration;
- approved oil specification and exact products already in the reservoir;
- the operating condition that produces foam, noise, or erratic movement; and
- inspection, sample, pressure, and flow findings that support the requested repair.
This information prevents a visually similar replacement from introducing a new inlet restriction, connection mismatch, filtration problem, or fluid incompatibility.
Conclusion
Concrete pump hydraulic oil foaming should be treated as a fluid-condition and circuit-evidence problem. First distinguish surface foam from entrained air, cavitation symptoms, and possible water contamination. Then trace the condition through oil level, suction integrity, inlet restriction, return-flow behavior, recent service work, and fluid identity.
Replacing the hydraulic pump, changing the oil, or adding antifoam before locating the entry or retention mechanism can hide the symptom temporarily while the root cause remains. A documented comparison before and after the repair is the most reliable way to close the diagnosis.