Concrete Pump Parts Knowledge
Concrete Pump Hydraulic Oil Selection: Viscosity, Compatibility, and Changeover Checks
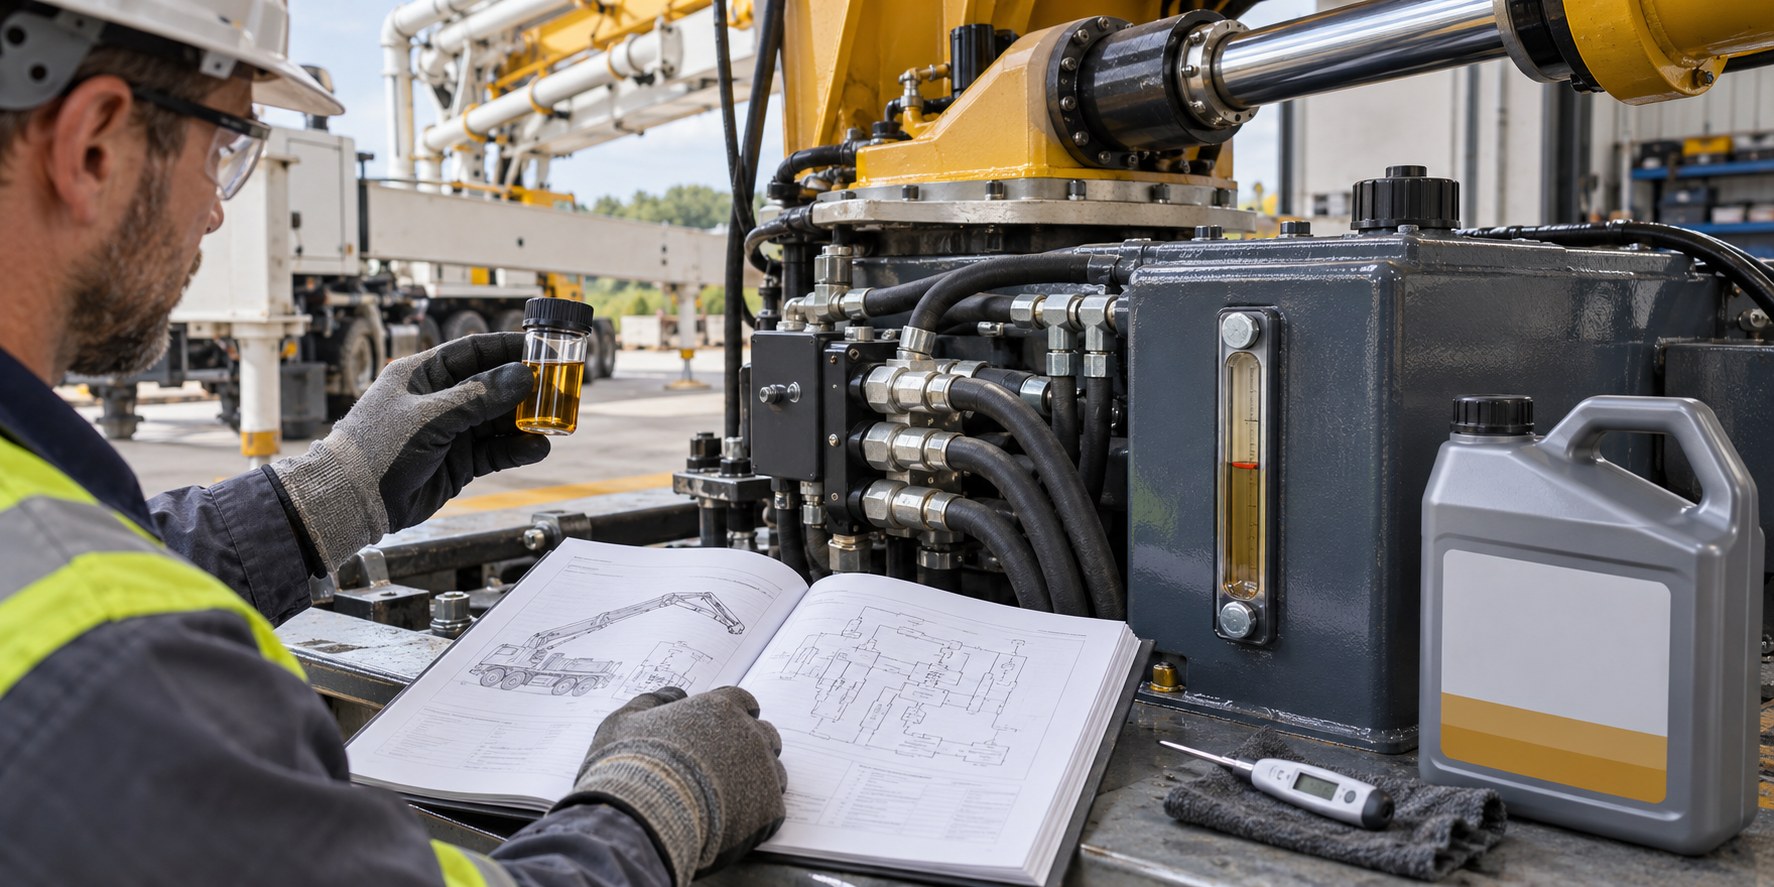
The correct hydraulic oil for a concrete pump is the fluid specified for the exact manufacturer, model, serial range, hydraulic components, and operating climate. A familiar label such as ISO VG 46 is not enough by itself. It identifies a viscosity class, but it does not prove that the base fluid, additive system, seal compatibility, cleanliness, or OEM approval is correct.
This distinction matters when a workshop is topping up an unfamiliar machine, changing oil for a different climate, or recommissioning a pump after repair. The wrong fluid may not cause an immediate failure. It can instead change cold-start suction, hot-oil leakage, valve response, air release, filter behavior, or seal performance, leaving a fault that appears only under temperature and load.
Why “ISO VG 46” is not a complete oil specification
ISO VG is a viscosity classification for industrial liquid lubricants. ISO 3448 establishes the classification system; the grade number is tied to kinematic viscosity at the reference temperature, not to every other property required by a hydraulic system. Two products carrying the same ISO VG number can differ in base stock, viscosity index, antiwear chemistry, detergency, air-release behavior, demulsibility, seal interaction, and formal equipment approval.
The letters printed before or beside the grade also matter. A manual may call for an HLP fluid under DIN 51524-2, an HM fluid under another classification, a named commercial product, or an OEM-approved list. Those descriptions should not be reduced to “46 oil.” DIN 51524-2, for example, defines minimum requirements for HLP hydraulic oils used where thermal stress, corrosion risk from water ingress, and antiwear performance are relevant.
An OEM may add restrictions beyond the base standard. Putzmeister’s 2024 approved-fluid bulletin uses HLP ISO VG 46 as its standard mineral-fluid specification for the pumps covered by that document, yet it also excludes several other fluid categories and zinc-free oils. That is a useful demonstration of the principle: matching the number 46 does not override manufacturer-specific chemistry or approval requirements.
How temperature changes the viscosity decision
Hydraulic oil becomes thicker as temperature falls and thinner as temperature rises. A grade that provides acceptable film thickness at operating temperature can create excessive inlet resistance during a cold start. A lower-viscosity grade that improves cold flow may become too thin at the hottest component or case-drain location. Selection therefore has to cover the complete temperature envelope, not only the daytime ambient temperature.
Consider four different temperatures:
- Minimum cold-start temperature: the oil in the reservoir and suction line before circulation begins.
- Normal stabilized reservoir temperature: useful for trending, but not necessarily the hottest point in the circuit.
- Local component temperature: pump housings, case drains, throttling valves, and high-leakage components can be hotter than the tank.
- Maximum permitted machine temperature: an OEM limit involving the complete system, not merely the oil’s flash point or marketing temperature range.
Putzmeister’s bulletin illustrates why grades cannot be changed informally. For the machines covered, it lists ISO VG 46 as standard, with ISO VG 32 and ISO VG 68 assigned different application ranges and corresponding machine-temperature adjustments. Those figures are Putzmeister-specific instructions, not a universal concrete-pump selection chart. Another pump may use different pumps, valves, seals, cooling capacity, software limits, or approved products.
Schwing-Stetter likewise emphasizes viscosity behavior across temperature, cleanliness, and condition-based oil analysis for its hydraulic oil. The practical conclusion is not that one brand’s oil is always necessary; it is that temperature performance and condition control belong to the equipment specification rather than to a generic shop rule.
What happens when the oil is too thick or too thin?
Oil that is too thick at startup can restrict the suction path, increase pressure drop through filters and passages, delay actuator response, and make the hydraulic pump harder to fill. Noise or sluggish movement during a cold start can be consistent with excessive viscosity, but the same observations can also come from low oil level, a restricted suction strainer, a clogged breather, air entry, or an unsuitable startup procedure.
Oil that is too thin at operating temperature can increase internal leakage and reduce the lubricating film in pumps, valves, and cylinders. A function may slow or lose force as the machine warms, yet that pattern does not prove the viscosity grade is wrong. Worn clearances, a passing relief valve, hot-oil conditions, or internal leakage in an actuator can produce similar symptoms.
For the valve-shift circuit, fluid behavior can affect the response of the directional valve, accumulator circuit, and Concrete Pump Slewing Cylinders. Even so, slow or irregular switching should be diagnosed as a circuit problem. Confirm command timing, pressure supply, restrictions, mechanical load, oil temperature, and actuator leakage before changing fluid or ordering a cylinder.
| Observation | Possible fluid-related mechanism | What to verify before concluding |
|---|---|---|
| Pump noise mainly after a cold start | Viscosity may be high at the suction condition | Specified grade, actual oil temperature, reservoir level, breather, suction path, warm-up procedure, and pump inlet condition |
| Valve or cylinder response slows as oil warms | Lower hot viscosity may expose internal leakage | Operating temperature, approved viscosity range, pressure/flow test, cylinder bypass, valve leakage, and pump condition |
| Temperature rises after a recent oil change | Wrong grade, incompatible mixture, aeration, or filter restriction may be involved | Product identity, retained old fluid, filter numbers, oil level, foam, cooler operation, and hydraulic load |
| New seals swell, harden, or begin leaking | Fluid chemistry may be incompatible with the elastomer | Seal material, new and previous fluid families, cleaning agents, temperature history, and written compatibility evidence |
These are diagnostic branches, not acceptance criteria. The equipment and component manufacturers must define the permissible viscosity and temperature limits.
Can different hydraulic oils be mixed?
Do not assume that two hydraulic oils can be mixed because both containers show the same viscosity grade. Mixing can alter additive balance, air release, water separation, filterability, seal behavior, or deposit formation. Bosch Rexroth guidance advises generally avoiding the mixing of fluids from different manufacturers or different fluid types and checking compatibility with the components and seals. It also notes that residues inside a replacement component can create an unintended mixture.
A small top-up and a complete changeover are different maintenance decisions. Before topping up, identify the oil already in the reservoir from records, a labeled sample, supplier documentation, and the machine specification. Color alone is unreliable: age, oxidation, dye, contamination, and previous mixing can all change appearance.
If the existing product cannot be identified, do not use a convenient fluid merely to restore the sight-glass level. Record the shortage, investigate leakage or consumption, consult the OEM or an oil specialist, and decide whether sampling, draining, compatibility testing, or a controlled changeover is required.
Mineral, biodegradable, and fire-resistant fluids are not simple substitutes
Concrete pumps may operate where environmental rules or fire risk affect the fluid choice. Biodegradable synthetic-ester fluids and water-containing or water-free fire-resistant fluids have different behavior from conventional mineral hydraulic oil. Their use can change seal selection, temperature limits, pump ratings, filtration, water control, disposal, and changeover requirements.
Putzmeister’s current bulletin, for example, separately addresses approved HEES biodegradable fluids and HFC fire-resistant fluid for specified applications. It also states a different maximum operating-temperature requirement for the HFC case described. That information must not be transferred to a different make or model, but it shows why “environmentally friendly 46” or “fire-resistant 46” is not a sufficient purchase description.
A fluid-family conversion may leave old oil in cylinders, hoses, accumulators, coolers, manifolds, and case-drain lines. The required residual limit and flushing method must come from the OEM, component suppliers, and fluid manufacturer. The replacement fluid should not be used as an improvised cleaning agent without an approved plan. Where a component failure has released debris, the separate question of hydraulic-system flushing after component failure must also be addressed.
A practical hydraulic-oil selection workflow
- Identify the machine exactly. Record manufacturer, model, serial number, pump-kit version, market, and any hydraulic-system modification.
- Obtain the current controlling documents. Use the applicable operating manual, service bulletin, approved-fluid list, hydraulic-pump data, and warranty requirements. A manual for a similar model is discovery evidence, not authorization.
- Document the existing fluid. Record product name, supplier, batch if available, fill date, top-ups, oil-analysis history, and whether a different fluid may remain in repaired components.
- Define the temperature envelope. Include minimum cold start, expected ambient range, stabilized reservoir temperature, duty cycle, cooler condition, and any OEM derating or control-limit change.
- Match the complete specification. Confirm fluid family, viscosity grade, performance standard, OEM approval, additive restrictions, seal/material compatibility, and required cleanliness—not just brand or viscosity.
- Plan filling and filtration. Use clean transfer equipment, the specified filter method, sealed containers, and protected fill points. New oil is not automatically clean enough for the installed hydraulic components.
- Set a verification baseline. Record oil level under the specified machine condition, sample location, temperature, pressure or response observations, filter status, and any oil-analysis targets before returning to full duty.
If the machine has a history of bubbles, milky oil, or unstable level, complete the hydraulic-oil foaming and aeration diagnosis before blaming viscosity. If it runs hot, use a thermal diagnostic sequence rather than selecting a thicker grade as a shortcut; the existing hydraulic-oil overheating workflow separates heat generation from inadequate heat rejection.
Information for Buyer Confirmation
When requesting oil, a top-up recommendation, or a fluid-change proposal, provide enough information for the supplier to confirm suitability in writing.
| Information to provide | Why it affects the decision |
|---|---|
| Concrete-pump make, model, serial number, year, and market | Separates model generations, regional specifications, and superseded manuals |
| Current OEM fluid specification and approved-product list | Defines more than viscosity and may exclude certain chemistries |
| Installed hydraulic pump, valve, accumulator, and actuator information | Identifies the most sensitive component and material requirements |
| Existing oil brand, product, grade, fluid family, and service history | Supports top-up compatibility or changeover planning |
| Minimum startup and maximum operating conditions | Tests whether viscosity remains suitable across the real temperature range |
| Seal and hose materials where a fluid family changes | Prevents assuming elastomer compatibility |
| Required cleanliness code, transfer filtration, and sample plan | Controls contamination introduced during filling |
| Reason for the change: climate, availability, failure, contamination, environmental rule, or fire risk | Determines whether a top-up, drain, flush, component inspection, or full conversion is needed |
Common questions
Is AW 46 the same as HLP 46?
Not automatically. The labels come from different naming conventions and may indicate broadly similar antiwear mineral hydraulic oils, but interchangeability depends on the product data sheet, the controlling standard, additive restrictions, OEM approval, and written compatibility confirmation.
Can ISO VG 32 be used in winter and ISO VG 68 in summer?
Only when the manufacturer authorizes those grades for the exact pump and specifies any required control-limit or operating changes. Seasonal swapping also creates a mixing and changeover question. Ambient temperature alone does not define the viscosity inside the hottest or coldest hydraulic component.
Can thicker oil cure weak pumping or a slow S-valve?
No oil grade should be used as a substitute for diagnosis. Thicker oil may temporarily reduce leakage in a worn component while increasing cold-start restriction and filter pressure drop. Identify the command, pressure, flow, temperature, leakage, and mechanical-load evidence first.
Should hydraulic oil be changed on a fixed hour interval?
Follow the machine’s current maintenance schedule and fluid-condition requirements. Some OEM guidance uses oil analysis rather than one universal interval. Severe contamination, water ingress, overheating, oxidation, an incompatible top-up, or destructive component failure can require action before a routine interval.
Conclusion
Selecting concrete-pump hydraulic oil is a specification-matching task, not a choice between three numbers on a shelf. Confirm the exact machine, fluid family, viscosity-temperature behavior, performance standard, OEM approval, material compatibility, cleanliness requirement, and changeover method. That record protects the hydraulic pump, valves, accumulators, hoses, filters, and cylinders—and makes later troubleshooting far more reliable.
Technical references
- Putzmeister, Approved Hydraulic Fluids for Concrete Pumps, CT 4748-5 EN
- ISO 3448:1992, Industrial Liquid Lubricants — ISO Viscosity Classification
- ASTM D2422-24, Classification of Industrial Fluid Lubricants by Viscosity System
- DIN 51524-2:2017-06, HLP Hydraulic Oils — Minimum Requirements
- Schwing-Stetter, Hydraulic Oils
- Bosch Rexroth, Hydraulic Fluid Selection and Requirements