Concrete Pump Parts Knowledge
Concrete Pump Hydraulic Oil Contamination: Sampling, ISO Codes, and Water Checks
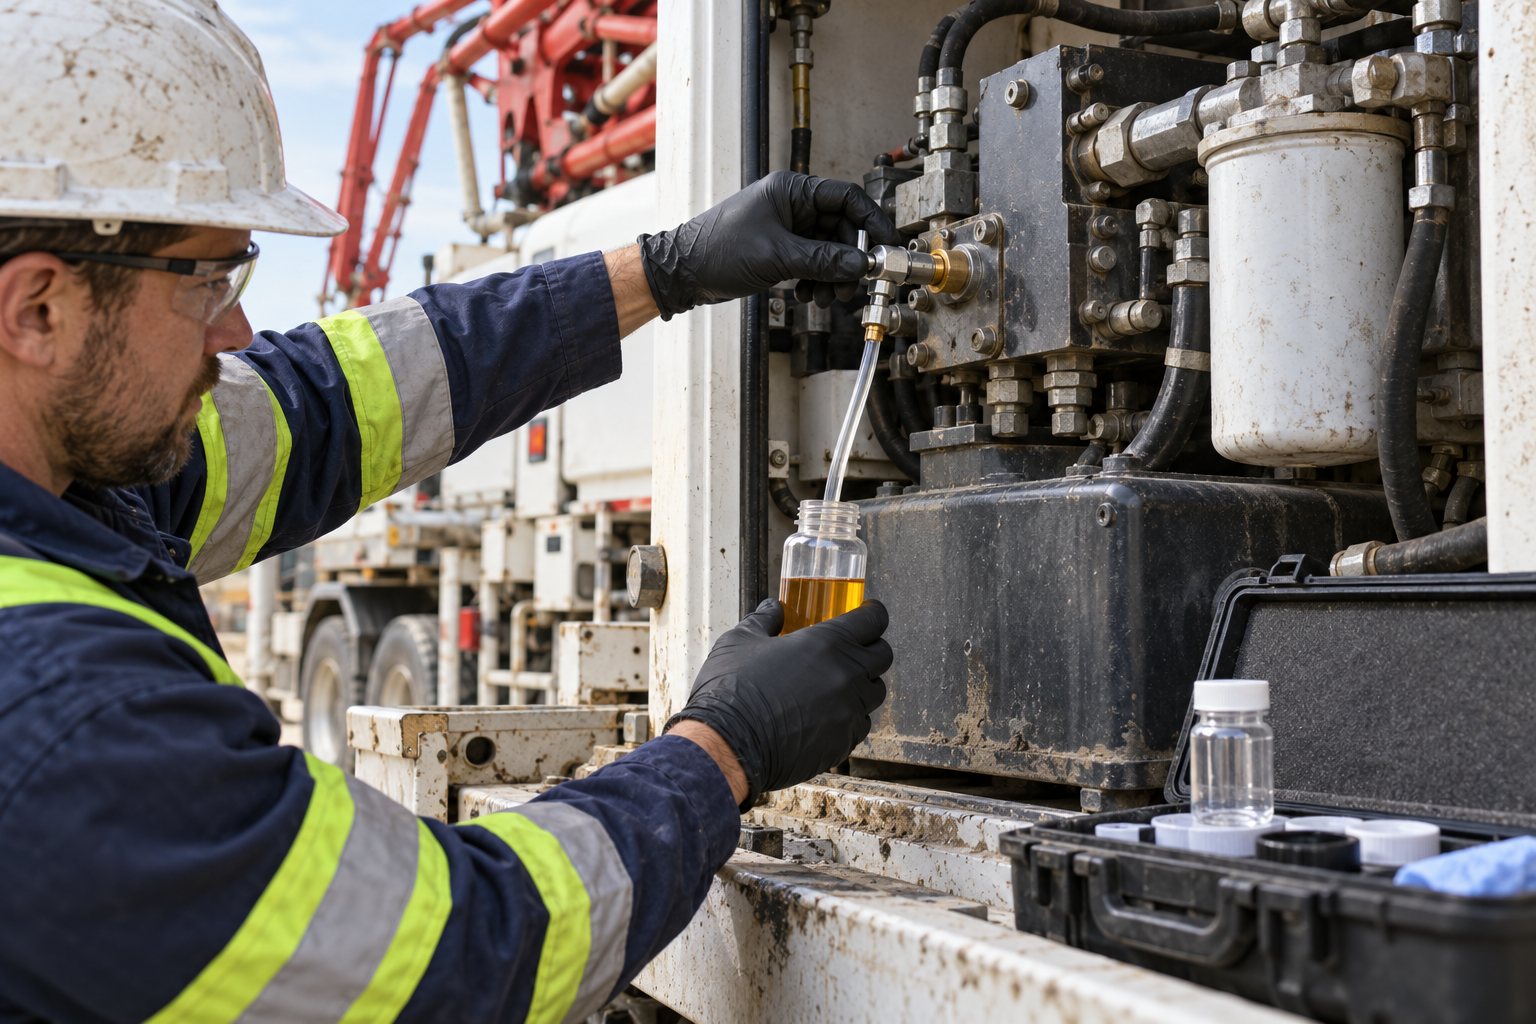
Concrete pump hydraulic oil contamination should be diagnosed from a representative oil sample, not from reservoir color alone. A particle count can quantify solid contamination, Karl Fischer testing can measure water, and viscosity or elemental analysis can help distinguish fluid deterioration from wear debris or the wrong oil. The result is useful only when the sample location, machine condition, oil hours, and applicable OEM target are recorded.
This matters because a concrete pump can continue cycling while fine contamination is abrading pump surfaces, valve clearances, and actuator seals. Conversely, a cloudy sample, a filter warning, or slow valve switching does not prove one root cause. The maintenance task is to move from observation to evidence without introducing contamination during sampling.
What Counts as Hydraulic Oil Contamination?
Contamination is not limited to visible dirt. A concrete pump hydraulic system may contain several different unwanted conditions:
- Solid particles from dust ingress, dirty transfer equipment, assembly residue, hose deterioration, corrosion, or component wear.
- Water in dissolved, emulsified, or free form. Entry paths can include condensation, a damaged filler-breather seal, wash water, poor storage, or a cooler fault where designs place oil and coolant or water across a heat-transfer surface.
- Another fluid introduced during top-up or component replacement. An incompatible fluid may change viscosity, additive behavior, seal compatibility, air release, or filterability even if the mixture looks clear.
- Air caused by suction leakage, low reservoir level, return-flow disturbance, or poor air release. Air is not solid contamination, but bubbles can make oil cloudy and can interfere with optical particle counting.
- Oil degradation products created by heat, oxidation, or additive depletion. These soft contaminants may contribute to deposits and may also complicate particle-count interpretation.
These conditions require different tests and different corrective actions. Treating every cloudy sample as water, or every high particle count as proof that the filter is too coarse, can send the repair in the wrong direction.
Why Visual Inspection Is Not Enough
Milky or hazy hydraulic oil can indicate dispersed water, but appearance alone cannot measure water content or identify the entry path. Fine air bubbles, mixed fluid, dye, oxidation products, and suspended debris can also change appearance. Clear oil is not evidence of acceptable cleanliness because damaging particles can be smaller than the eye can resolve.
Visual inspection is still useful. Record color, clarity, foam, sediment, odor, and whether the sample changes after standing. These are screening observations that help the laboratory and technician select the next test. They are not a substitute for a particle count, water measurement, or comparison with the specified fluid.
| Observation | Possible explanations | What to verify before acting |
|---|---|---|
| Milky or opaque oil | Emulsified water, persistent aeration, mixed fluid | Karl Fischer water result, sample after controlled circulation and de-aeration, fluid identity |
| Foam at the reservoir | Air ingress, return disturbance, low level, unsuitable or mixed oil | Suction path, level under the OEM test condition, return arrangement, fluid approval |
| Dark oil | Oxidation, overheating, suspended fine material, mixed oil | Viscosity, acid number or oxidation indicators, temperature history, reference sample |
| Visible metallic debris | Active component wear, previous failure residue, poor post-repair cleaning | Filter and magnetic-plug evidence, elemental or wear-debris analysis, affected circuit |
| Unexpectedly high particle count | Real contamination, dirty bottle, unpurged sample port, water droplets or air affecting the counter | Repeat sample from the same live point, sampling method, laboratory comments, water content |
What Does an ISO 4406 Cleanliness Code Tell You?
ISO 4406:2021 provides a code for the quantity of solid particles in hydraulic fluid. A three-part result such as 18/16/13 reports cumulative particle-count ranges at 4 micrometres and larger, 6 micrometres and larger, and 14 micrometres and larger, using the calibrated particle-size convention identified by the test method.
The code is a concentration classification, not a diagnosis. It does not identify whether particles are steel, silica, elastomer, rust, or oxidation residue. It also does not establish one universal cleanliness target for every concrete pump. The acceptable target depends on the most contamination-sensitive components, system pressure, control-valve design, OEM requirements, and the measurement method.
A result should therefore be compared with the pump manufacturer’s current requirement for that model and fluid, not with an arbitrary internet chart. Component data can be informative, but the assembled machine may have a different required cleanliness level. The trend from the same machine, sample point, and operating condition is usually more useful than a single isolated number.
How Should a Concrete Pump Hydraulic Oil Sample Be Taken?
The sample must represent oil circulating in the system. ISO 4021 identifies extraction from a main flow line of an operating system as the preferred approach for particulate analysis; reservoir sampling is an alternative when a suitable sampler is not fitted. A bottom drain can over-represent settled debris, while oil skimmed from the top may under-represent circulating contamination.
Follow the model-specific operating and safety procedure. Do not loosen a pressurized fitting to improvise a sample point. Hydraulic injection injuries can be severe, and a concrete pump may contain stored pressure even after the engine stops.
Use a Repeatable Sampling Sequence
- Identify the machine and fluid. Record pump model, serial number, oil product, oil hours, machine hours, top-up history, recent repairs, filter changes, and the reason for sampling.
- Stabilize the condition. Sample at the temperature and operating state specified by the OEM or laboratory plan. The aim is to suspend representative contamination without creating an unsafe operating condition.
- Use the designated point. A permanently installed sampling valve at a documented live zone gives more repeatable results than a drain plug or an unmarked hose connection.
- Clean and purge the port. Clean the exterior, connect the approved adapter, and discard the specified purge volume so stagnant oil and debris from the valve cavity do not dominate the sample.
- Protect the bottle. Use a laboratory-approved clean container. Do not rinse it with shop solvent, touch the inside of the lid, or place the lid face-down.
- Fill without splashing. Keep the tube and bottle clear of dirty machine surfaces. Leave the headspace required by the laboratory so the sample can be mixed before analysis.
- Label immediately. Record the exact sample point, date, oil temperature if available, operating state, and technician. “Hydraulic tank” is often too vague for trend analysis.
- Keep future samples comparable. Use the same point and similar operating conditions. A trend loses value when one sample comes from a live return line and the next comes from a cold reservoir drain.
If the first result is surprising and no urgent failure evidence exists, a repeat sample is often the correct next step. It is cheaper than draining a large system because of a contaminated bottle or an unpurged valve.
Which Tests Answer Which Maintenance Question?
| Test | What it can establish | What it cannot establish by itself |
|---|---|---|
| Automatic particle count / ISO 4406 code | Quantity distribution of particles in the reported size channels | Particle material, exact source, or whether a component has failed |
| Karl Fischer water test | Water concentration under the stated method | Where the water entered or whether corrosion has already occurred |
| Viscosity at a stated temperature | Whether the used oil differs materially from the expected viscosity | Whether the difference came from mixing, shear, oxidation, or the wrong initial fill |
| Elemental spectroscopy | Concentrations of reported elements that may relate to wear, additives, or dirt | The identity and size of every particle or the failed component without context |
| Microscopy, patch test, or wear-debris analysis | Particle shape, color, approximate type, and presence of larger debris | A complete system diagnosis without operating and component evidence |
| Acid number, FTIR, or other fluid-condition tests | Evidence relevant to oxidation, contamination, or additive condition | A universal oil-change limit without an OEM or lubricant baseline |
For water measurement, ASTM D6304 specifies coulometric Karl Fischer titration for petroleum products, lubricating oils, and additives. For particle counting, the laboratory method and sample preparation matter. Water droplets, air bubbles, or soft contamination can affect optical results, so particle count and water content should be interpreted together when the sample is hazy.
How Do You Trace the Contamination Path?
Start with the type of evidence, then inspect plausible entry or generation points. Avoid changing several things at once before collecting evidence; otherwise the original cause can disappear while the system remains vulnerable.
When Solid Particle Counts Are High
Check the filter indicator under the correct oil-temperature condition, filter-element identity, bypass condition, service history, and the cleanliness of recent top-up equipment. Review any hose, pump, valve, or cylinder work completed since the last normal sample. New oil should not be assumed clean merely because it came from a sealed drum; transfer pumps, hoses, and containers can add contamination.
A more restrictive filter is not automatically the solution. Media efficiency, flow capacity, cold-start pressure drop, housing bypass, collapse rating, and OEM approval must be compatible. The separate LeeIndust guide to hydraulic filter bypass and replacement checks explains why a physical fit does not confirm filter suitability.
When Water Is Elevated
Inspect the filler-breather and its seal, reservoir openings, washdown exposure, outdoor storage, and any heat exchanger or water-adjacent component permitted by the specific machine design. Compare the sample with weather, storage, and service records. A desiccant breather may help in a humid, cycling environment, but it cannot repair a direct rainwater path or remove a large existing water load.
The article on the concrete pump hydraulic tank breather covers restriction, moisture control, and replacement matching. If contamination followed a component failure or incompatible-fluid event, the required scope may extend beyond a tank drain because cylinders, hoses, coolers, manifolds, and accumulators retain fluid. See the separate hydraulic-system flushing guide for cleanup planning.
When Wear Metals or Large Debris Increase
Relate the material evidence to the circuit and symptoms. A particle report cannot by itself distinguish a main pump from a cylinder, valve, motor, or old repair residue. Examine filter media, magnetic collectors where fitted, case-drain trends if the OEM procedure permits, actuator drift tests, and component-specific inspection results.
In the valve-shifting circuit, contaminated oil can accelerate wear at close-clearance valves and dynamic seals. Before condemning Concrete Pump Slewing Cylinders, separate cylinder bypass from control-valve leakage, mechanical binding, pressure-supply faults, and contamination-related sticking. Replacing the actuator without cleaning the circuit can expose the new seals and bore to the same debris.
Does a Bad Result Mean the Oil Must Be Replaced?
Not necessarily. The corrective method depends on the contaminant, severity, fluid condition, system design, and cause.
- Moderate solid contamination with healthy fluid: approved off-line filtration may restore cleanliness, provided the ingress or wear source is controlled.
- Water contamination: water-absorbing media, vacuum dehydration, controlled oil replacement, or a more extensive cleanup may be appropriate depending on the water form and quantity. A standard particulate element is not automatically a water-removal device.
- Wrong or incompatible fluid: a controlled changeover may require more than draining the reservoir. Confirm residual-fluid tolerance, seal compatibility, and the OEM process.
- Active component failure: repair the source, replace affected filters, and clean retained volumes before recommissioning. Filtering the reservoir while a component continues generating debris will not close the problem.
- Questionable sample: repeat the sample before choosing an expensive corrective action, unless safety or failure evidence requires immediate shutdown.
After corrective work, take a verification sample under the same documented condition. A “clean” post-service bottle is not meaningful if it was collected before trapped contamination circulated back from the rest of the system.
Information for Buyer Confirmation
When requesting oil-analysis service, sampling hardware, off-line filtration, or replacement hydraulic components, provide enough data for the supplier to match the task rather than guess from a photograph.
- Concrete pump manufacturer, model, serial number, and hydraulic schematic revision if available.
- Fluid brand, product name, viscosity grade, base-fluid family, approval, fill volume, and service hours.
- Current OEM cleanliness target and water limit, if specified.
- Exact sample point, port type, available pressure, temperature, and safe access condition.
- Required laboratory tests and reporting standard, including the ISO 4406 edition or other code system.
- Recent filter, hose, pump, valve, accumulator, cooler, or cylinder work.
- Symptoms, alarm history, filter-indicator behavior, and previous analysis reports.
- For filtration equipment: reservoir volume, fluid viscosity range, desired cleanup target, connection method, flow limit, power supply, and water-removal requirement.
Practical Questions
Does milky oil always mean water?
No. Milky oil is a strong reason to test for water, but persistent aeration, an incompatible mixture, or suspended degradation products can also create haze. Confirm water with an appropriate test and investigate the entry path.
Can a filter warning prove that the oil is dirty?
No. A differential-pressure or contamination indicator can respond to loaded media, high viscosity during cold operation, incorrect element selection, or a restriction elsewhere in the housing. Check it under the OEM-specified condition.
Is one ISO cleanliness code enough to approve the machine?
No. Compare the result with the machine target, water content, fluid condition, prior trends, filter evidence, and any active symptoms. A low particle count does not prove correct viscosity or fluid compatibility.
Should the sample come from the reservoir drain?
Usually not for a routine circulating-fluid trend. A drain sample may be intentionally useful when investigating settled debris or water, but it should not be compared as though it were the same as a live-line sample.
Conclusion
Concrete pump hydraulic oil contamination is best managed as an evidence chain: take a representative sample, select the test that answers the actual question, compare the result with the correct machine requirement, trace the contamination pathway, and verify the cleanup. This approach prevents both underreaction to invisible contamination and expensive overreaction to an ambiguous visual symptom.
Technical Sources
- ISO 4406:2021 — Hydraulic fluid power — Fluids — Method for coding the level of contamination by solid particles
- ISO 4021:1992 — Extraction of fluid samples from lines of an operating system
- ASTM D6304-25 — Water in petroleum products, lubricating oils, and additives by coulometric Karl Fischer titration
- Donaldson — Hydraulic Filtration Overview
- Putzmeister P 715 operating instructions
- Schwing S 20 original operating instructions — hydraulic fluid purity classification